Part 1 — MECHANICAL FEATURES OF TYPE
Reading edition
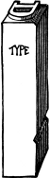
Printing owes its development first and chiefly to movable metal types. The so-called invention of printing was the discovery of a method of making serviceable type in quantity. The idea of a separate type for each letter of the alphabet was probably conceived long before Gutenberg’s time, but it remained for him and his associates to devise an apparatus for making them quickly and accurately enough to be of practical value. That apparatus was the type mold, which experience has since proved to be the most efficient means of securing exactness and uniformity in a number of small pieces of metal.
Type is made of an alloy of lead, tin, and antimony. Its length (technically called height-to-paper) is .918 of an inch. Each type is cast separately in a mold, and has the letter or printing character in bold relief on one end.
Exact uniformity of body is necessary in order that the types, when composed in lines and pages, may be locked together by pressure at the sides so as to make a compact mass. All types in a printing form must be of the same height, so that their faces may present a uniformly level surface from which an impression may be made that will show all the characters clearly. A short type will print faintly or will not print at all, while a long one will be unduly forced into the sheet.
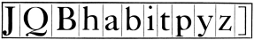
There are on an average about one hundred and fifty roman letters and other characters required in ordinary book printing. These letters are divided into a number of classes: full-body letters, ascending letters, descending letters, short letters; and in some cases, small capitals, which are larger than short letters but not so tall as capitals or ascenders. Only a few letters, like J and Q, cover nearly the entire surface on the end of the type; other letters, like B h l i, cover the upper portion chiefly and leave a blank space at the bottom; while the small letters, like a e o u v, occupy only the middle portion of the surface; still others, like g y p, cover the middle and lower portions of the surface. As all these irregular shapes must be made to appear in line with each other, the type-body on which they are made is larger than the letter. The blank parts around the face of a letter are called the counter, the shoulder, and the beard. The counter is the shallow place between the lines of the face. The shoulder is the low flat part of the type around the face. The beard is the sloping part between the face and the shoulder.
A A, the face B B, the serifs C C, the counter E, the pin-mark F F, the beard G, the shoulder H, the nick J J, the feet K, the groove
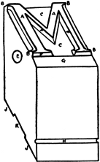
An important feature of a type is the nick on the side of the body. In many cases there may be two, three, or even four nicks on a type. Usually all the types of a font have nicks that are identical in number and position, and when the types are composed in lines these nicks match each other and form continuous grooves on the lower part of the line of type.
The nicks serve as guides to the compositor when taking the type from the case to his composing stick, and they assist in distinguishing the types of one font or face from those of another on the same size of body.[1] Individual letters of different type faces sometimes bear such close resemblance that they are more readily distinguished by the nick or some other body-mark than by the face. A difference in alignment of nicks in a line will readily show the presence of a wrong-font letter. Typefounders sometimes make an extra nick on a few small-capitals (o s v w x z) in order to distinguish these types from the lower-case letters of the same font.
A Font of Type
A font of type is an assortment of one size and kind that is used together. It is usually all the type in the composing-room of a certain kind matching in body, nick, and face. A small font may be held in one case, but several cases may be required for a font of large quantity.
An ordinary font of roman type for book work will include these characters:
Roman Capitals—A B C D E F G H I J K L M N O P Q R S T U V W X Y Z Æ Œ
Small Capitals—a b c d e f g h i j k l m n o p q r s t u v w x y z æ œ
Lower-case Letters[2]—a b c d e f g h i j k l m n o p q r s t u v w x y z æ œ fi fl ff ffi ffl
Figures—1 2 3 4 5 6 7 8 9 0 (or oldstyle )
Marks of Punctuation—Period . comma , colon : semi-colon ; hyphen - apostrophe ’ exclamation mark ! question mark ? parenthesis ( bracket [ The latter two are used in pairs () [], the second type being set in reversed position.
Quotation Marks are made by two inverted commas “ at the beginning and two apostrophes ” at the end of the quoted matter. In some fonts there is a double mark |"| |"| cast on single bodies, but these are not often used.
Dashes—En – em — two-em —— three-em ———
Reference Marks—Asterisk or star * dagger † double dagger ‡ section § parallel ‖ paragraph ¶ index (hand, or fist) ☞
Braces—Two-em three-em pieced braces made on em bodies, which may be extended more or less with dashes


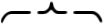
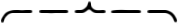
The dollar-mark $, short-and (or round-and) &, and sterling pound-mark £ are also included with all full fonts.
The character is an old-style ligature (two joined letters cast on one type) made in some fonts of old-style faces. It is one of the many letter combinations formerly common, in imitation of the work of old manuscript writers.

Many styles of roman types have italic letters to match, but the italic fonts include only capitals, lower-case, figures, and punctuation marks:
Italic Capitals—A B C D E F G H I J K L M N O P Q R S T U V W X Y Z Æ Œ
Italic Lower-case—a b c d e f g h i j k l m n o p q r s t u v w x y z æ œ
Italic Figures—1 2 3 4 5 6 7 8 9 0 ()
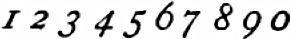
Italic Points, etc.[3]—. , : ; - ’ ! ? ) $ &
Small capitals are not made for italic fonts, except in rare cases. When they are needed in composition, capitals of a smaller size of type are justified into the text line.
Other extra characters, not included in ordinary fonts but which may be added when required, are accented letters (â é ë ī ō û etc.), fractions ¾ 5⁄13 etc.), mathematical signs (+ × ÷ = etc.), superior (ab 42) and inferior (ab 12) letters and figures, leaders (…………), commercial signs (@ ℔ ⅌ ℀ ¢), and many other characters for special kinds of printing.
Fonts of advertising, jobbing, and display types usually consist of the capitals, lower-case letters, figures, and points, with occasionally a few extra characters. For many recent styles of heavy faces the founders furnish fractions, accented letters, and other special characters to match in boldness of face, but these are not included in ordinary letter-fonts.
The quantity of each character apportioned to a regular font is the estimated average required for ordinary composition in the English language. It is rare that more than a fraction of a small font can be used in any piece of composition. No general scheme can meet the needs of every kind of work; tables and statistical matter will need extra figures, directories and other lists will call for surplus capitals, dialogue matter will need more than the usual portion of commas and apostrophes for quote-marks; even plain descriptive composition will often call for extra “sorts.” For these and other peculiar kinds of composition extra quantities of some characters, as well as other material, must be provided.
Ordinary roman and other faces used in large quantities are measured by weight. The proportion of letters in a 100-pound font, showing the proportions of each character, is given on the next page. Miscellaneous faces used in small quantities are put up in fonts containing a certain number of each letter, the size of the font being designated by the number of capital A’s and lower-case a’s it contains.
Scheme for 15-A 30-a Job Font of 12-Point[4]
CAPITALS A15 B6 C10 D8 E18 F7 G7 H8 I15 J5 K5 L10 M8 N15 O15 P8 Q3 R15 S15 T15 U8 V5 W6 X3 Y6 Z3 &6 LOWER-CASE a30 b12 c16 d18 e40 f12 g12 h20 i30 j8 k8 l20 m16 n30 o30 p12 q6 r30 s30 t30 u16 v8 w12 x6 y12 z6 fi3 fl3 ff3 ffi2 ffl2 POINTS period31 comma31 colon6 semi-colon6 hyphen9 apostrophe13 !9 ?8 (6
FIGURES 15 24 34 44 54 64 74 84 95 06 $4 £5
A WEIGHT FONT
Proportion of Letters &c. in 100 lb. of Roman Type
CAPITALS oz A8½ B5 C7½ D6½ E10 F5 G5½ H6½ I6 J4½ K4 L6 M7½ N7½ O7½ P6 Q2½ R8 S8 T9 U5 V3½ W7 X2 Y4½ Z2 ƾ Œ¾ &3½ ——— 10 lb SMALL CAPS. oz A2½ B1½ C2 D2 E3½ F1½ G1½ H2 I1¾ J1¼ K1¼ L2 M2¼ N2½ O2½ P1¾ Q¾ R2¼ S2¼ T2½ U1½ V1 W2 X¾ Y1¼ Z½ Ƽ Œ¼ &1 ——— 3 lb LOWER CASE lboz a46 b1- c114 d3- e68 f11 g14 h38 i212 j-5 k-8 l18 m210 n46 o44 p16 q-5 r35 s36 t312 u22 v-14 w110 x-5 y14 z-4 æ-1 œ-1 fi-5 ff-4 ffi-4 fl-3 ffl-3 —————— 5812 FIGURES oz 18 26½ 35½ 45 56½ 65 75 85 95 010 $2 £½ ——— 4 lb
POINTS lboz period1- comma 18 colon -2 semi-colon-3 hyphen-9 apostrophe-4 !-2 ?-2 —-3 (-2 [-1 —————— 44
TOTALS lb Capitals10 Small Capitals3 Lower-case58¾ Figures4 Points4¼ Spaces and quads20 ——— 100 lb SPACES AND QUADS lboz hair-2 5-to-em -10 4-to-em 1- 3-to-em6- en-quad24 em "110 2-em "42 3-em "44 —————— 20 lb
Weight fonts of body type are usually put up by the founders in sections or parts of fonts as given in the above summary of totals, so that one or more of these sections may be obtained to supplement a font already in use.
It will be noted that braces, dashes, and reference-marks are omitted in the above list. These characters, like fractions, commercial signs, etc., are not now considered parts of ordinary fonts, but are put up in separate packages and must be specially ordered when wanted.
Font schemes apportioned in quantities like the foregoing are more or less closely adhered to for original packages of foundry-cast type. To insure precision, when ordering, it is necessary to state not only the quantity (by number of letters or weight) but also whether a complete font or part of a complete font (capital font, lower-case font, or figure font) is referred to.
The Sizes of Type
All printing type has, first, a name denoting its size, and second, one denoting the style of its face. For instance, the type used for the text of this book is 10-point (its size) Lining Caslon Oldstyle (the foundry name of its face).
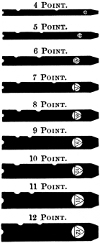
The size of a type is the vertical thickness of its body—the thickness of a line up and down the page. The width of a type is its set. Thus a 12-point en-quad is 12-point body and 6-point set, a 10-point figure of the thickness of an en quad is 10-point body and 5-point set, etc. The total length of a type, including feet and face, is its height-to-paper.
American type sizes conform to a graduated scale known as the point system. The unit of the system is a division of space called a point, which is .0138+ (approximately 1⁄72) of an inch. Type bodies are multiples of this point.
The usual sizes are graduated by points up to 12-point. Sizes above 18-point are multiples of 6-point up to 60-point (18, 24, 30, 36, 42, 48, 54, 60). Larger sizes are 72-point, 84-point (rare), 96-point, 120-point, and 144-point, the latter being the largest type commonly cast in a mold.
The above squares show one em of the sizes stated. The letters show the size of face made on the body.
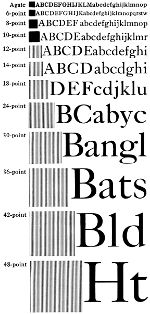
In addition to the small sizes shown in the accompanying illustration, there are some intermediate sizes like 5½-point and 4½-point, and type as small as 3-point has been made. These are rare, however, as type smaller than 5½-point is not practicable for extended use. These small sizes are employed for special purposes, like miniature editions of books (parts of the Bible, prayer books, etc.) cut-in notes, piece-fractions, small borders, special characters, and occasional words or lines that are required to be put in the smallest possible space. The size of type known as agate (fourteen lines to an inch) is considered the common standard of measurement for newspaper and magazine advertising space.
Many plain types for books, periodicals, etc., are made only in small sizes. Certain faces are made in a few sizes only, while others are made in more or less complete series from 6-point to 48-point. The irregular sizes of 5½-point, 7-point, 9-point, and 11-point are mostly roman faces, with companion italics, and a few bolder styles for headings and other display in combination with romans of the same body. Many new faces are now made by founders in graded series from 6-point to 72-point, and in some cases even larger. Type faces adapted to many kinds of work are made in nearly all the regular sizes, while those faces designed for small and dainty work, like personal and society cards and stationery, are made only in the smaller sizes of the list.
Types are now often cast with faces larger or smaller than is commonly made on the body, such as a 12-point face on 10-point body, giving the effect of compactness; or an 8-point face made on a 10-point body, which gives a lighter appearance as if opened with 2-point leads. These are known as bastard types. Because of this irregularity in the faces of types it is difficult to know the exact body-size of a type by merely examining a printed sheet.
Borders, ornaments, florets, and decorative characters cast on type-bodies are now made mostly in sizes based on the 6-point as the unit (6, 12, 18, 24-point, and larger multiples), but 8-point, 10-point, and 14-point sizes are sometimes used.
Before the adoption of the point system, type sizes were named in a haphazard way. Arbitrary names were given to certain sizes and in many cases types of the same name made by different founders varied so much in size that they could not be used together without great inconvenience to the printer. Some of these old names still survive and are applied to the point-system bodies which approximate the old sizes.
POINT SIZEOLD NAME
3-point …excelsior
4-point …brilliant
4½-point …diamond
5-point …pearl
5½-point …agate
6-point …nonpareil
7-point …minion
8-point …brevier
9-point …bourgeois
10-point …long primer
11-point …small pica
12-point …pica
14-point …english
16-point …columbian
18-point …⎰ great primer ⎱ three-line nonpareil
20-point …paragon
22-point …two-line small pica
24-point …two-line pica
28-point …two-line english
32-point …two-line columbian
36-point …two-line great primer
40-point …two-line paragon
44-point …meridian
48-point …canon, four-line pica
While these old names and their sizes are now nearly obsolete, young printers should learn the names and associate them with their corresponding sizes of the point system. In the foregoing list there are several intermediate sizes (16, 20, 22, 28, 32, 40, 44-point) rarely used for type of recent design. Fonts of these odd sizes may be sometimes found, and there has been a size of 15-point made, but little used. These odd sizes are, however, mostly old faces, scripts, and black-letter, originally cast on old bodies and later, after the introduction of the point system, made on new point-bodies which are nearest to their original sizes.
The point system has been applied to the width of types, as well as to the body-size; that is, the set of each type is fixed at a given number of points or fraction thereof. This method simplifies in a degree the process of accurate justification, as each line, though containing various letters and spaces, is composed of the same number of units. An advantage over the old method of unrelated widths is in the saving of time in composition, by reducing the number of different widths in the characters of the alphabet. By the old method each type had its own special width; in a complete font there might be a hundred or more different widths. By the modern point system those characters which are nearly alike in width are made on the same set, or, if different, the variation is governed by the standard unit.
Lining Type Faces
Showing irregular alignment of faces, the old method. Showing exact alignment of different faces, the modern way.
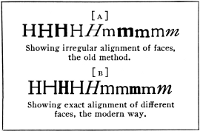
American founders have adopted the practice of casting type-faces on uniform lining systems, variously known as American line, standard line, uniform line, etc. The earlier practice was to cast the type of a font so that the letters would align at the bottom only with their mates of the same font, without reference to any other face of type. When the compositor had occasion to use two or more different faces of type in the same line, these faces were rarely in even alignment, but were irregularly high or low, as shown in the accompanying example [a]. This lack of uniformity made it necessary when a different face was used in the line, as is often required in jobbing and advertisements, to use thin leads, cards, or pieces of paper above and below different parts of the type-line in order to get the faces in line—an operation more or less troublesome and expensive. By the modern lining system, the faces made on any given size of body are cast to align with each other, as shown in the second example [b]. These different faces require no more adjustment than if they were all of one font.
On different sizes of type the shoulder, or blank space, at the bottom of the letter increases gradually with the size of the type, so that a word of small type placed beside a larger size must have some spacing material below as well as above to keep it in its right alignment. This necessary difference in the face-alignment of various sizes is graduated by points, in the lining system, so that when more than one size type is used in the same line the justification is made by using point-body leads. This makes the use of slips of card and paper unnecessary and secures greater accuracy and solidity of the composed page.
30-point to 6-point lined up with 1-point.
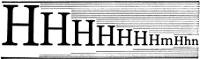
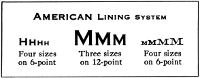
Faces of radically different style are not, however, all cast on the same alignment, but are classified into three groups. One group embraces the majority of type-faces, those having capitals and small letters, g y p j. Another group embraces fonts of capitals only, mostly faces known as title letters and combination lining faces which, having no descenders, may be made lower on the body. A third group includes those faces having long descenders, like script types, which must be placed high on the body.
These types show letters cast on [a] the common line, [b] title line, [c] script line.
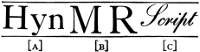
A common class of “lining” types for job work are the combination series, or those having two or more sizes of face (capitals only) cast on bodies of the same size. Each face is made to line with the others on the same body, and all the faces are readily used in combination, with a single size of spaces and quads. In order that the type of each face may be readily distinguished, the nicks are varied in number or position—a single nick for one face, two nicks for another, etc.
American Lining System
Kerned Types
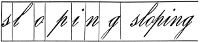
When the face of a letter is so large that it projects over the type-body, it is known as a kerned type. Letters of this kind are common in italic and script fonts, and there are a few letters, like f and j, in some oldstyle roman fonts which have the tip of the letter overhang. Kerned types are a source of trouble because of the ease with which these projections break off during composition, proofing, etc. Yet they cannot be entirely dispensed with, especially in italic and script faces having a definite slope, where the long letters would have wide gaps on the side (as shown in the script line above) if they were cast on bodies wide enough to hold the entire face. In some styles of upright faces having extra long descending letters g, p, q, y, these descenders may be kerned.
Showing why some letters must be made on kerned types.
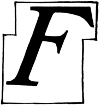
Large italic letters are sometimes mortised at the corners, instead of kerned, to allow the next letter to fit close.
Modern type-makers try, by changing the shape of the letters slightly, to avoid kerns as much as possible, because of the extra care and expense involved in casting. Too often, unfortunately, this avoidance of the kern, in order to meet mechanical convenience, is secured by sacrificing the distinctive form of the letter.
Spaces and Quads
Short metal spaces and quads (from quadrat, a square), used for blanks between words and elsewhere, are of various thicknesses, as illustrated below. An em is a square of type body of any size. This 10-point em □ is ten points square; a 10-point three-to-em space is one third of the em, a four-to-em is one fourth, etc. The en quad is really a thick space, though called a quad, and is equal to half the em. Larger blanks are the two-em and three-em quads, used to fill the last lines of paragraphs and other wide spaces.
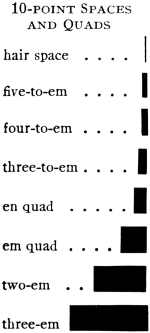
The metal blanks shown here are the regular spaces and quads belonging to a font of type of the size of 10-point. They enable the compositor to obtain the many different spacings required to make lines the required length, and to properly separate words and place them wherever desired in the line. While these thicknesses of spaces are the usual kinds for sizes of type up to 12-point, larger types may have other kinds of spaces, six-to-em, eight-to-em, and even smaller divisions. The thickness of the hair space does not always bear the same proportion to the em quad; in some sizes it is one sixth of the em, in others it may be one eighth or one twelfth. Very thin spaces (copper ½-point, brass 1-point), for exact spacing and justifying, are supplied by dealers.
A space of the thickness intermediate between the three-to-em and the en quad, known as a patent space, has been made for use in book work. Although it has great advantage as a substitute for two of the thinner spaces when these are needed in spacing a line, its use has been limited and it is not included with the usual assortment furnished by dealers.
The common spaces and quads for general work, when the type itself is used for printing, are about seven-eighths of the height of the type, so that they are well below the printing surface. A type-page composed with these spaces will have a little deep hole at the top of each space. These numerous little holes present a difficult surface for making a good wax mold when an electroplate is made for printing. Where much molding is to be done, higher spaces, quads, and other blanks are provided. These high spaces and quads reach nearly to the shoulder of the type.
How Type is Made
Solid lines indicate one half of the mold. Dotted lines show the other half in position. Shaded portion represents type metal filling aperture in the mold. The molten type metal flows through the opening at A, down to the side B, where the matrix (not shown in this diagram) molds the face of the type. The tag of metal, called the jet, marked C, is cut off after casting. D is a narrow flange on the mold which forms the nick on the under surface of the type body.
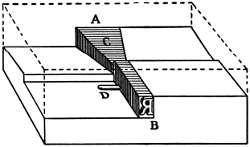
The mold in which type is cast consists of two essential parts—the steel box in which the body is formed, and the matrix which contains a sunken image of the character. The matrix covers the opening at one end of the mold, and on the opposite end (which is the foot of the type) is an opening through which the melted metal is injected. A mold is made for a single body-size of type but it is adjustable sideways to correspond to the various widths of the letters in an alphabet. One mold may be used to cast, in succession, all the letters of a font of type, or it may be used to cast any number of fonts of different faces that may be made on the same body, by merely changing the matrices that form the face. The mold is made in two sections, which are fitted together so as to close up to the required width of the letter, and, after the cast is made, to open slightly in order to release the type.
Matrix
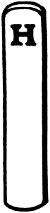
The Matrix. There are three different methods of making type matrices. By the oldest method the first step is to cut the character on the end of a small bar of soft steel, called a punch; when this is done, the steel is hardened and it is used to stamp an impression in a bar of copper. This copper bar is a matrix in the rough, and its sides are next trimmed and squared so that it will fit the mold.
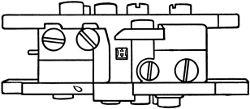
Type-mold complete, in two parts, but without the matrix (which is shown separately above). Position of the matrix when cast is made is indicated by the letter H on the end of the type within the mold. The upper and lower halves of the mold slide horizontally, to make the interior casting-box wide or narrow to conform to the required widths of various letters.
The second method of making a matrix is by electrotype process. The original pattern of the letter may be engraved by hand or by other operation, or it may be a perfect type-face of a previous casting. This is fitted into a small frame of brass and then held in the vat of an electro-galvanic battery, which deposits a thick film of copper around the pattern and fills the opening in the brass frame. When this electro-plating process is completed, the pattern letter is extracted and the brass frame, with its copper impression of the letter, becomes the essential feature of the matrix. It is then reinforced by riveting another plate on the back, and is trimmed and fitted to place on the mold.
A third process of making matrices is with an automatic matrix-cutting machine, in which the shape of the desired letter is cut in the face of a plate of composition metal by a small rapidly-revolving cutting point. A large pattern of the letter is placed in one part of the machine, and while the operator traces the outline with the point of a lever all the motions are duplicated in miniature by the cutting tool on the bar of metal, which becomes, when completed, a matrix.
Casting the Type. The old-time method of casting type was with hand molds, the melted metal being poured in at the foot of the mold with a small ladle while the mold was held in the hand. In the modern casting machine, the mold with its matrix, is assembled by the side of the metal pot, in which the metal is kept at a uniform temperature by means of a gas furnace.
In the center of this metal pot is a rod with a spring attachment which, at each operation of the machine, acts as a plunger to force a small stream of hot metal through a side aperture into the jet-hole of the mold. After the casting, the two parts of the mold separate slightly, the matrix is drawn away from the face of the type, and the cast is moved out; then the mold and matrix close together again and the operation is repeated. Cold water or air is circulated near the mold to keep an even temperature. The matrix for one character only is placed in the machine and when enough types have been cast, it is taken out and replaced by another, the change usually requiring but a few moments.
There are several kinds of type-casting machines in use, such as hand casters, steam casters, and automatic casters. The older style is the hand caster, which is operated by a small wheel with a handle attached. Steam casters are operated by mechanical power (originally steam power).
When type is cast by a hand machine it is unfinished, as a piece of metal called the jet still adheres to the bottom of each type. This jet is broken off, and the types are set in long lines and fastened in a narrow channel, face down. A small plane smooths away the rough surface caused by breaking off the jet. This leaves a shallow groove on the bottom of each type and allows it to stand squarely on its feet. The types also have slight burs and sharp edges of metal which must be rubbed off before they are ready for inspection and for the font-room. Type cast on the older “steam” machines require the jet to be broken off after the casting, and the final finishing of the type is done afterward by other operations. These finishing touches are done mostly by hand, with the aid of a polishing stone or a small dressing wheel.
On the automatic machine, which is the modern method of casting type, breaking off the jet, rubbing, dressing, etc., are all accomplished automatically on the machine, the types coming out in a continuous line practically ready for the compositor’s case.
The foregoing describes in a general way the methods of making type by the regular founders. There is now a great deal of type made by automatic composing and casting machines installed directly in many composing rooms.
Two distinctive styles of these machines are now extensively used—the Linotype and the Monotype. Both of these have reached a high degree of efficiency because of their nice mechanisms, based on the principle of automatically operated molds, matrices, and delivery devices.
In the Linotype the matrices for a desired line of words are assembled side by side and the line is cast in one piece.
In the Monotype the mechanism automatically and rapidly adjusts the matrix of the desired letters one at a time over the mold, and each type is cast and moved along into lines and then into a column on a galley.
The Linotype
Four-Magazine Linotype Machine
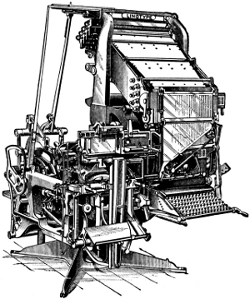
The Linotype (line-o’-type) consists of a mechanism for assembling brass dies or matrices in lines, presenting them in front of a mold in which a type-high metal bar, or slug, is cast, and returning the matrices to their respective channels for use again. The brass matrices have the characters of the alphabet, figures, points, etc., sunk into their edges; these are held in a magazine, which is an arrangement of channels in an inclined position above a keyboard. By the pressing of a key the required matrix is released, which drops and is carried into place by a small belt. Wedge-shaped space-bands are also controlled by a key, and when sufficient matrices and space-bands are assembled to make the line a bell rings. By operating a lever the line of matrices then moves in front of the mold inserted in the side of a wheel and behind which is a pot of melted metal.
By the next operation the space-bands are pushed between the words, thus spreading them to the measure. The line justified, a plunger in the metal-pot forces a quantity of metal into the mold and against the line of matrices, forming a metal strip or slug with the letters in relief on one edge. After the cast is made, a turn of the mold-wheel and other mechanism shaves off the surplus metal on the foot of the slug and pushes it between knife-edges, where it is trimmed on the sides, and is then pushed on to a galley. The melting of the metal is done by a small gas furnace under the metal-pot.
After the matrices have been used for the line they are lifted by an arm to the top of the machine and distributed again, each character in its particular channel in the magazine. The matrices for each character have a set of notches or teeth different from every other character; and as they are moved along the distributing apparatus by horizontal screws each matrix reaches a point where its notches are matched and it drops into the top of its channel. There are a number of matrices of each character, and the arrangement of the machine is such that three lines of matrices may be kept in operation at once—one being assembled, one at the casting mold, and the third being distributed.
The work of the operator is to manipulate the keyboard and, at the end of each line, move a lever which engages the mechanism that carries the assembled line to the mold. All other operations are performed by mechanical power.
The Monotype
Monotype Keyboard
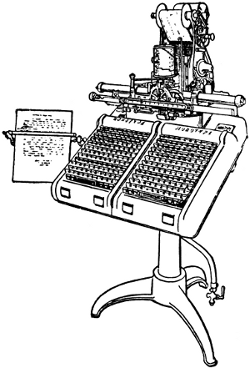
The Lanston Monotype is a type-casting machine which produces separate types set in lines of any length, up to sixty ems pica, spaced and justified. It is in two parts—a keyboard and a casting machine. The function of the keyboard section is to punch a series of holes in a moving strip of paper, which unwinds from one spool to another, passing under a series of punches in its journey. The punches are operated by pressing the keys on the keyboard, the result of this operation being a roll of perforated paper ribbon. This ribbon is then taken to the casting machine, which contains a pot for melted metal, a stationary mold for the size of type to be cast, and a matrix-plate. The matrix-plate is about five inches square, and has on its face depressed images or matrices of each letter and character of the font. The perforated strip of paper, when fed to its place, controls the movement of the matrix-plate, so that the required letter is adjusted exactly in place over the mold, while the melted metal is squirted in to form the type. The type then moves away and takes its proper place in the line, until the line is completed, when it is automatically moved out on to a galley.
The Monotype keyboard, being an entirely separate machine, may be and usually is operated in any place away from the casting apparatus and work may be executed on it anytime before casting. The perforated roll may be fed through any number of times to produce duplicate castings of the matter, and a matrix-plate for a different face may be used if desired. In the casting of the line the proper spaces are cast with it, the spacing needed to justify each line being indicated on the perforated record during composition on the keyboard.
Monotype Casting Machine
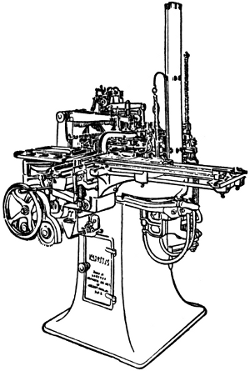
A peculiarity of Monotype composition is that, while the keyboard produces the perforated roll in the usual sequence from beginning to end of the story, the casting machine reverses the process by starting at the end of the composition and finishing up with the beginning.
Ingredients of Type Metal
The metal used for casting type is a mixture of lead (five parts), antimony (two parts), tin (one part), and sometimes a small addition of copper. Lead forms the chief part of all type metal, as it melts easily and fuses readily with other metals; but lead alone is too soft for the service required of type. Antimony is brittle and gives hardness, and tin is added to impart toughness. Lead and antimony in approximately these proportions make an alloy which has the unusual quality of expanding slightly, instead of shrinking, when cooling, thus permitting a full, sharp cast in all parts of the mold. Tin flows readily when melted and increases the smoothness of the cast on the surface of the mold. A small quantity of copper may sometimes be added to give still greater toughness.
The metal used for small sizes of type is commonly harder than that used for the large sizes, the softness of the metal gradually increasing with the size of type made. Script types and faces with delicate lines are usually cast with metal a little harder than that used for the normal and bolder faces.
The foregoing refers more particularly to type cast by the regular foundries. The metal used in automatic casting machines, like the Monotype, contains a larger proportion of lead and less antimony; while the metal used for casting line-slugs in the Linotype machine is composed of still larger proportion of lead and very little of the other two metals. Stereotype metal and metals used for leads, slugs, furniture, etc., are largely lead.
Wood Type
Large types, such as are used for posters and large bills, are made of wood. The smallest size for practical use is 48-point, or 4-line pica. Sizes of wood type are multiples of the pica, and are so named, as 8-line, 10-line, etc. They are much cheaper than metal types, though not as durable or satisfactory for printing. The wood commonly used is maple, and the letter is made on the end of the grain. It must be well seasoned and polished. Pine and other soft woods are used for very large sizes of wood type and poster engravings.
The manner of cutting the letter is by routing away the blank parts with a small rapidly-revolving cutter. The strip of wood, large enough to make several letters, and planed type-high, is placed in a machine equipped with a pantagraph apparatus. A pattern letter is put in place, and over this a guide-point is moved. On another part of the machine is the revolving cutting tool. As the guide-point is moved over the pattern its motions are duplicated on the block under the cutting tool, which cuts away the wood. When the letters on a block are thus routed out, they are sawed apart, the finishing touches given, and the letters oiled.