Chapter XV · FINISHING
Reading edition
CHAPTER XV. FINISHING
The finishing touches are added to the cloth after the latter leaves the loom. The first operation is that of inspecting the cloth, removing the lumps and other undesirables, as well as repairing any damaged or imperfect parts. After this, the cloth is passed through a cropping machine the function of which is to remove all projecting fibres from the surface of the cloth, and so impart a clean, smart appearance. It is usual to crop both sides of the cloth, although there are some cloths which require only one side to be treated, while others again miss this operation entirely.
A cropping machine is shown in the foreground of Fig. 41, and in this particular case there are two fabrics being cropped or cut at the same time; these happen to be figured fabrics which have been woven in a jacquard loom similar to that illustrated in Fig. 38. The fabrics are, indeed, typical examples of jute Wilton carpets. The illustration shows one of the spiral croppers in the upper part of the machine in Fig. 41. Machines are made usually with either two or four of such spirals with their corresponding fixed blades.
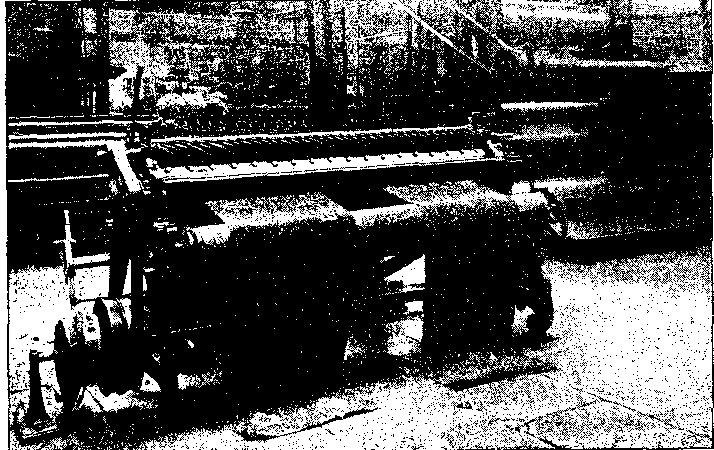
FIG. 41 CROPPING MACHINE AT WORK
The cloth is tensioned either by threading it over and under a series of stout rails, or else between two in a specially adjustable arrangement by means of which the tension may be varied by rotating slightly the two rails so as to alter the angle formed by the cloth in contact with them. This is, of course, at the feed side; the cloth is pulled through the machine by three rollers shown distinctly on the right in Fig. 42. This view illustrates a double cropper in which both the spirals are controlled by one belt. As the cloth is pulled through, both sides of it are cropped by the two spirals.[3] When four spirals are required, the frame is much wider, and the second set of spirals is identical with those in the machines illustrated.
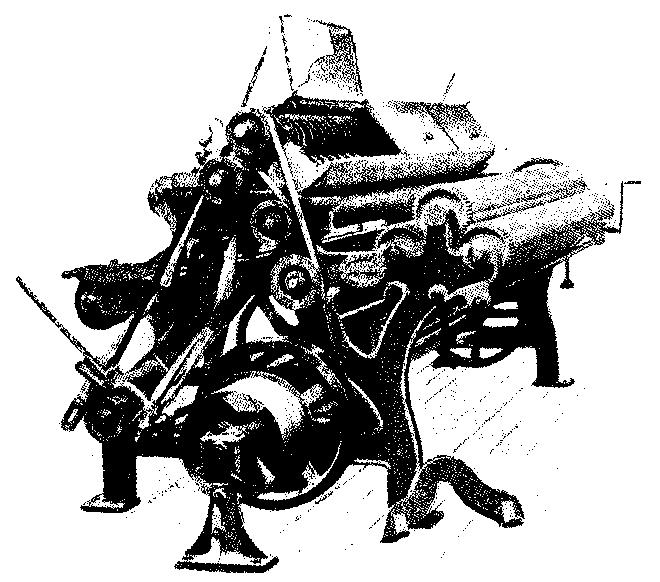
FIG. 42 DOUBLE CROPPING MACHINE By permission of Messrs. Charles Parker, Sons & Co., Ltd.
[Footnote 3: For a full description of all finishing processes, see The Finishing of Jute and Linen Fabrics, by T. Woodhouse. (Published by Messrs. Emmott & Co., Ltd., Manchester.)]
The cropped cloth is now taken to the clamping machine, and placed on the floor on the left of the machine illustrated in Fig. 43, which represents the type made by Messrs. Charles Parker, Sons &, Co., Dundee. The cloth is passed below a roller near to the floor, then upwards and over the middle roller, backwards to be passed under and over the roller on the left, and then forwards to the nip of the pulling rollers, the bottom one of which is driven positively by means of a belt on the pulleys shown. While the cloth is pulled rapidly through this machine, two lines of fine jets spray water on to the two sides of the fabric to prepare it for subsequent processes in which heat is generated by the nature of the finishing process. At other times, or rather in other machines, the water is distributed on the two sides of the cloth by means of two rapidly rotating brushes which flick the water from two rollers rotating in a tank of water at a fixed level. In both cases, both sides of the fabric are "damped," as it is termed, simultaneously. The damped fabric is then allowed to lie for several hours to condition, that is, to enable the moisture to spread, and then it is taken to the calender.
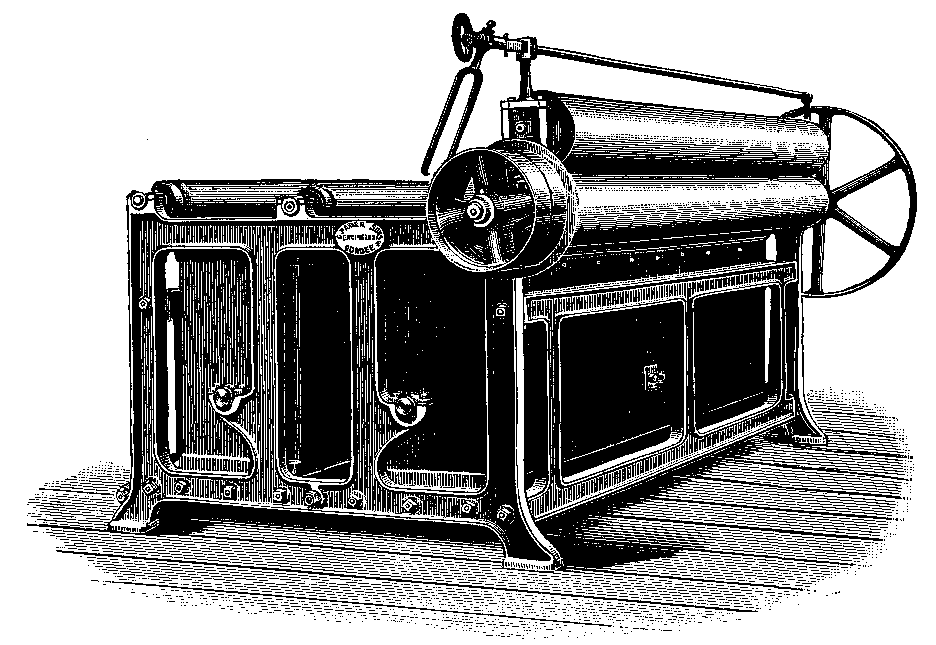
FIG. 43 DAMPING MACHINE By permission of Messrs. Charles Parker, Sons & Co., Ltd.
The calenders for jute almost invariably contain five different rollers, or "bowls," as they are usually termed; one of these bowls, the smallest diameter one, is often heated with steam. A five-bowl calender is shown on the extreme right in Fig. 41, and in the background, while a complete illustration of a modern 5-bowl calender, with full equipment, and made by Messrs. Urquhart, Lindsay & Co., Ltd., Dundee, appears in Fig. 44.
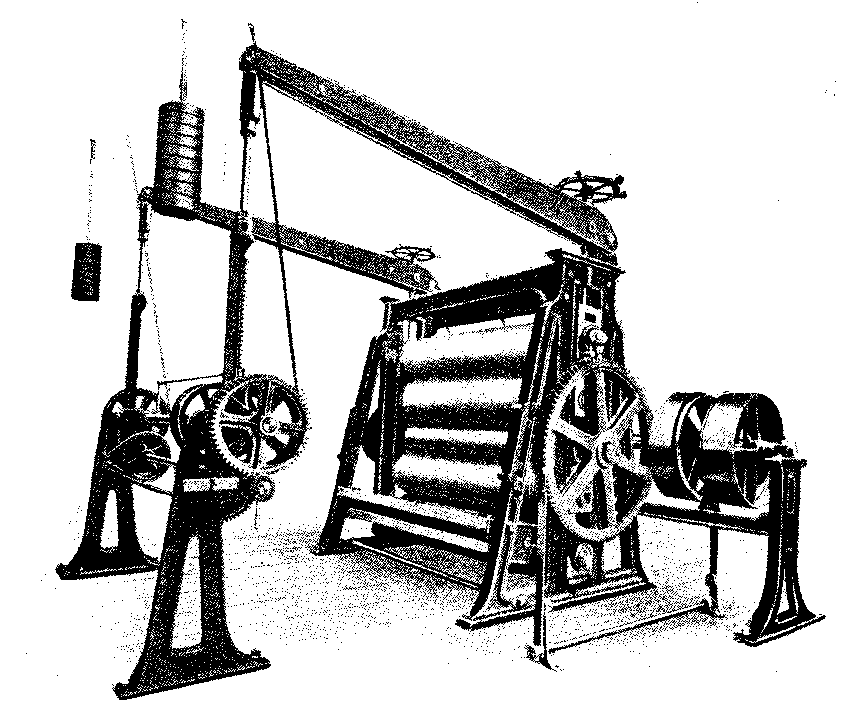
FIG. 44 CALENDAR
The cloth is placed on the floor between the two distinct parts of the calender, threaded amongst the tension rails near the bottom roller or bowl, and then passed over two or more of the bowls according to the type of finish desired. For calender finish, the bowls flatten the cloth by pressing out the threads and picks, so that all the interstices which appear in most cloths as they leave the loom, and which are exaggerated in the plan view in Fig. 34, are eliminated by this calendering action. The cloth is then delivered at the far side of the machine in Fig. 44. If necessary, the surface speed of the middle or steam-heated roller may differ from the others so that a glazed effect--somewhat resembling that obtained by ordinary ironing--is imparted to the surface of the fabric. The faster moving roller is the steam-heated one. For ordinary calender finish, the surface speed of all the rollers is the same.
Another "finish" obtained on the calender is known as "chest finish" or "round-thread finish." In this case, the whole length of cloth is wound either on to the top roller, or the second top one, Fig. 44, and while there is subjected to the degree of pressure required; the amount of pressure can be regulated by the number of weights and the way in which the tension belt is attached to its pulley. The two sets of weights are seen clearly on the left in Fig. 44, and these act on the long horizontal levers, usually to add pressure to the dead weight of the top roller, but occasionally, for very light finishes, to decrease the effective weight of the top bowl. After the cloth has been chested on one or other of the two top bowls, it is stripped from the bowl on to a light roller shown clearly with its belt pulley in Fig. 41.
There are two belt pulleys shown on the machine in Fig. 44; one is driven by an open belt, and the other by a crossed belt. Provision is thus made for driving the calender in both directions. The pulleys are driven by two friction clutches, both of which are inoperative when the set-on handle is vertical as in the figure. Either pulley may be rotated, however, by moving the handle to a oblique position.
The compound leverage imparted to the bearings of the top bowl, and the weights of the bowls themselves, result in the necessary pressure, and this pressure may be varied according to the number of small weights used. The heaviest finish on the calender, i.e. the chest-finish on the second top roller, imitates more or less the "mangle finish."
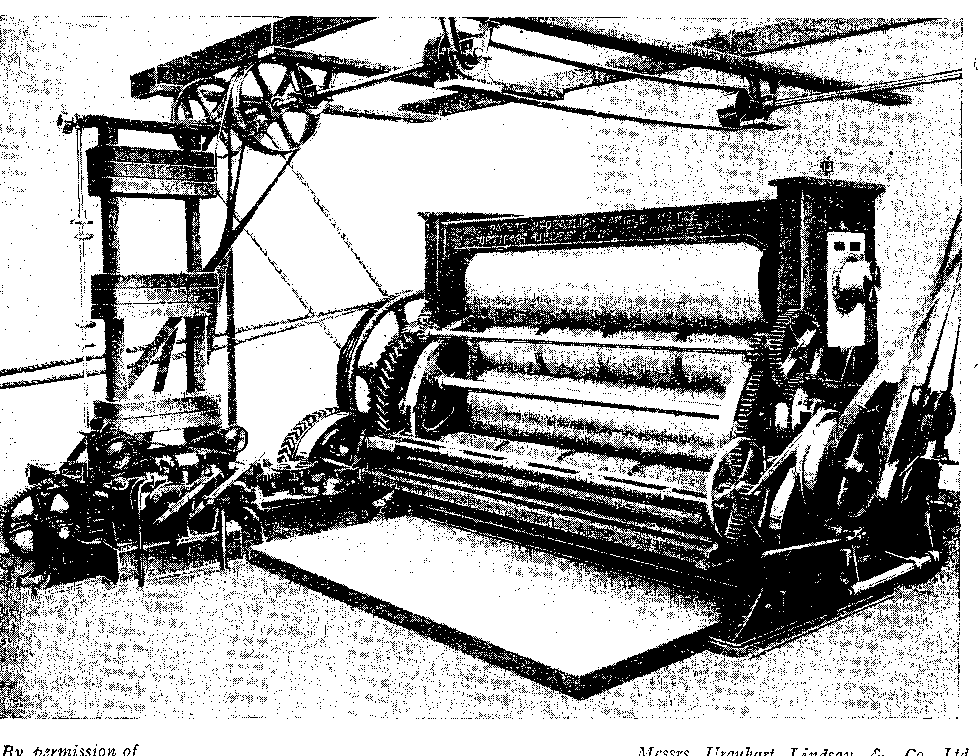
FIG. 45 HYDRAULIC MANGLE. By permission of Messrs. Urquhart, Lindsay & Co., Ltd.
A heavy hydraulic mangle with its accumulator and made by Messrs. Urquhart, Lindsay & Co., Ltd., Dundee, is illustrated in Fig. 45. The cloth is wound or beamed by the mechanism in the front on to what is termed a "mangle pin"; it is reality a thick iron bowl; when the piece is beamed, it is automatically moved between two huge rollers, and hydraulic pressure applied. Four narrow pieces are shown in Fig. 45 on the pin, and between the two rollers. There are other four narrow pieces, already beamed on another pin, in the beaming position, and there is still another pin at the delivery side with a similar number of cloths ready for being stripped. The three pins are arranged thus o°o, and since all three are moved simultaneously, when the mangling operation is finished, each roller or pin is moved through 120°. Thus, the stripped pin will be placed in the beaming position, the beamed pin carried into the mangling position, and the pin with the mangled cloth taken to the stripping position.
While the operation of mangling is proceeding, the rollers move first in one direction and then in the other direction, and this change of direction is accomplished automatically by mechanism situated between the accumulator and the helical-toothed gearing seen at the far end of the mangle. And while this mangling is taking place, the operatives are beaming a fresh set, while the previously mangles pieces are being stripped by the plaiting-down apparatus which deposits the cloth in folds. This operation is also known as "cuttling" or "faking." It will be, understood that a wide mangle, such as that illustrated in Fig. 45. is constructed specially for treating wide fabrics, and narrow fabrics are mangled on it simply because circumstances and change of trade from time to time demand it.
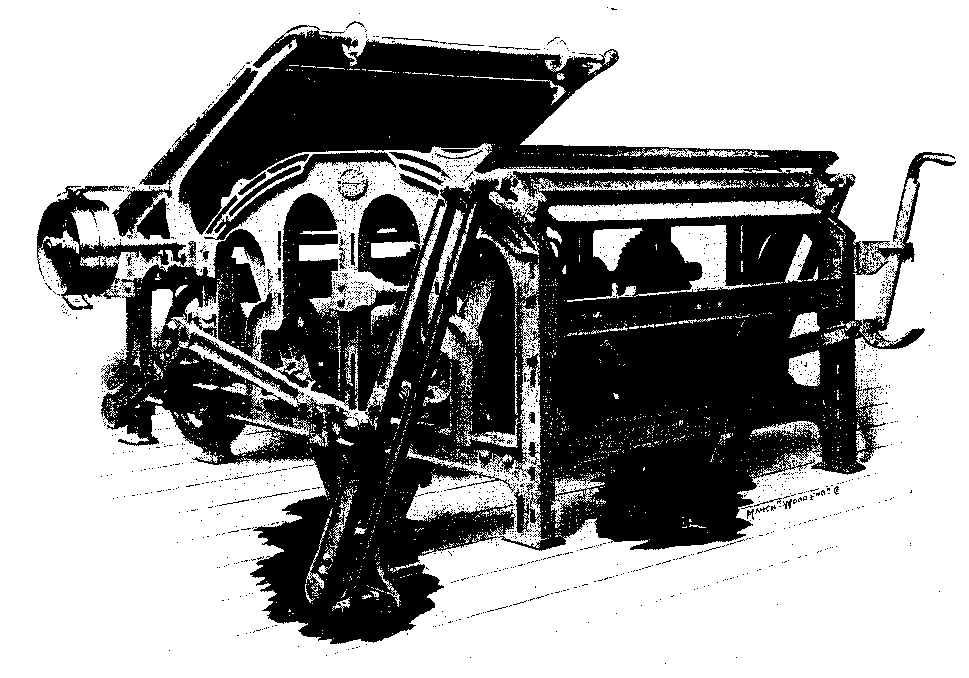
Fig 46 FOLDING, LAPPING OR PLEATING MACHINE By permission of Messrs. Charles Parker, Sons & Co. Ltd.
The high structure on the left is the accumulator, the manipulation of this and the number of wide weights which are ingeniously brought into action to act on the plunger determine the pressure which is applied to the fabrics between the bowls or rollers.
Cloths both from the calender and the mangle now pass through a measuring machine, the clock of which records the length passed through. There are usually two hands and two circles of numbers on the clock face; one hand registers the units up to 10 on one circle of numbers, while the slower-moving hand registers 10, 20, 30, up to 100. The measuring roller in these machines is usually one yard in circumference.
If the cloth in process of being finished is for use as the backing or foundation of linoleum, it is invariably wound on to a wooden centre as it emerges from the bowls of the calender, measured as well, and the winding-on mechanism is of a friction drive somewhat similar to that mentioned in connection with the dressing machine. Cloths for this purpose are often made up to 600 yards in length; indeed, special looms, with winding appliances, have been constructed to weave cloths up to 2,000 yards in length. Special dressing machines and loom beams have to be made for the latter kind. When the linoleum backing is finished at the calender, both cloth and centre are forwarded direct to the linoleum works. The empty centres are returned periodically.
Narrow-width cloths are often made up into a roll by means of a simple machine termed a calenderoy, while somewhat similar cloth, and several types of cloths of much wider width, are lapped or folded by special machines such as that illustrated in Fig. 46. The cloth passes over the oblique board, being guided by the discs shown, to the upper part of the carrier where it passes between the two bars. As the carrier is oscillated from side to side (it is the right hand side in the illustration) the cloth is piled neatly in folds on the convex table. The carriers may be adjusted to move through different distances, so that any width or length of fold, between limits, may be made.
Comparatively wide pieces can be folded on the above machine, but some merchants prefer to have wide pieces doubled lengthwise, and this is done by machines of different kinds. In all cases, however, the operation is termed "crisping" in regard to jute fabrics. Thus, Fig. 47, illustrates one type of machine used for this purpose, and made by Messrs. Urquhart, Lindsay & Ca., Ltd., Dundee. The full-width cloth on the right has obviously two prominent stripes--one near each side. The full width cloth passes upwards obliquely a triangular board, and when the cloth reaches the apex it is doubled and passed between two bars also set obliquely on the left. The doubled piece now passes between a pair of positively driven drawing rollers, and is then "faked," "cuttled," or pleated as indicated. The machine thus automatically, doubles the piece, and delivers it as exemplified in folds of half width. In other industries, this operation is termed creasing and, rigging. Some of the later types of crisping or creasing machines double the cloth lengthwise as illustrated in Fig. 47, and, in addition, roll it at the same time instead of delivering it in loose folds.
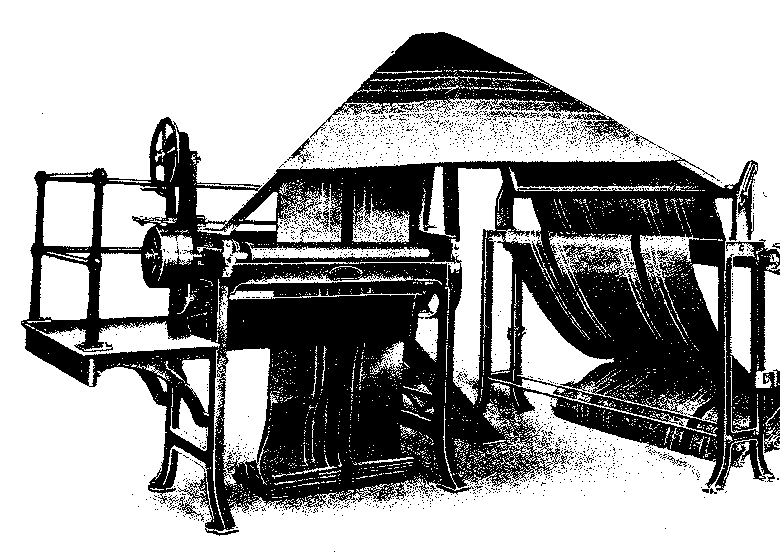
FIG. 47 CRISPING, CREASING OR RIGGING MACHINE By permission of Messrs. Urquhart Lindsay & Co. Ltd.
If the cloth is intended to be cut up into lengths, say for the making of bags of various kinds, and millions of such bags are made annually, it is cut up into the desired lengths, either by hand, semi-mechanically, or wholly mechanically, and then the lengths are sewn at desired places by sewing machines, and in various ways according to requirements.
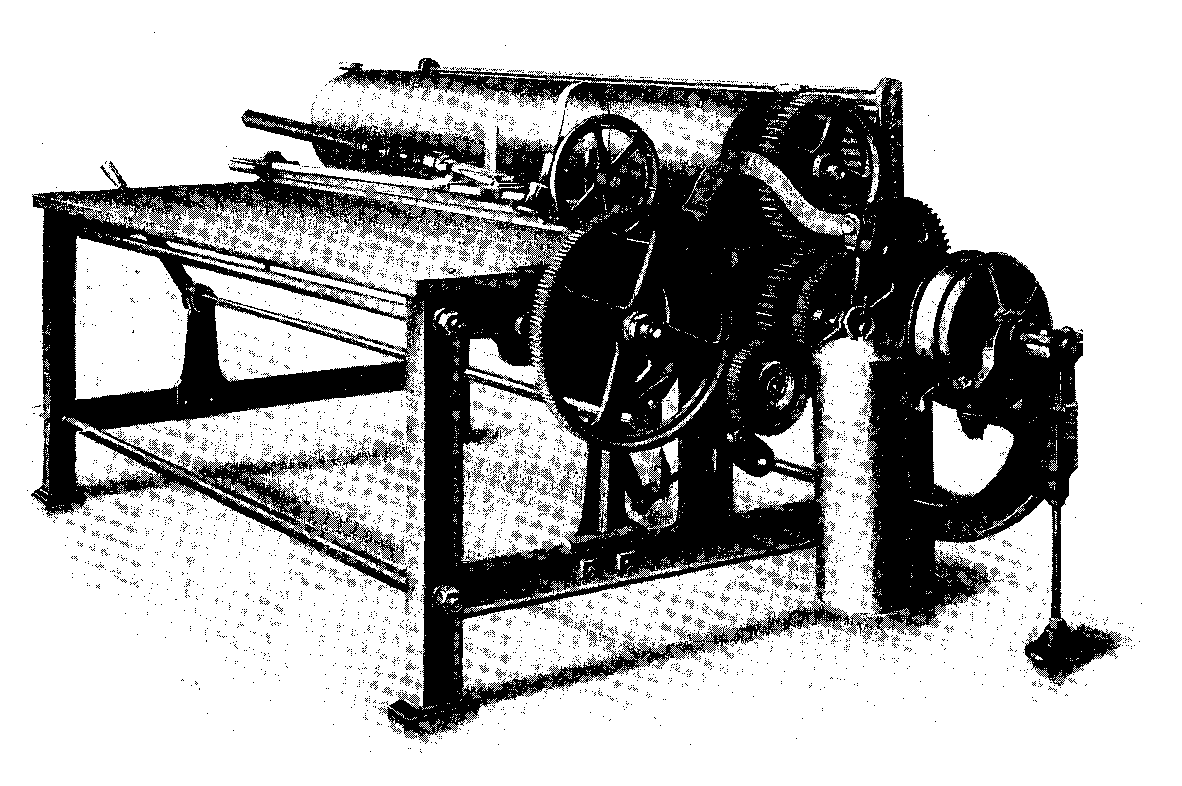
FIG 48 SEMI-MECHANICAL BAG OR SACK CUTTING MACHINE By permission of Messrs. Urquhart, Lindsay & Co. Ltd
Fig. 48 illustrates one of the semi-mechanical machines for this purpose; this particular type being made by Messrs. Urquhart, Lindsay & Co., Ltd., Dundee. About eight or nine different cloths are arranged in frames behind the cutting machine, and the ends of these cloths passed between the horizontal bars at the back of the machine. They are then led between the rollers, under the cutting knife, and on to the table. The length of cloth is measured as it passes between the rollers, and different change pinions are supplied so that practically any length may be cut. Eight or nine lengths are thus passed under the knife frame simultaneously, and when the required length has been delivered, the operative inserts the knife in the slot of the knife frame, and pushes it forward by means of the long handle shown distinctly above the frame and table. He thus cuts eight or nine at a time, after which a further length is drawn forward, and the cycle repeated. Means are provided for registering the number passed through; from 36,000 yards to 40,000 yards can be treated per day.
The bags may be made of different materials, e.g. the first four in Fig. 32. When hessian cloth, II, Fig. 32, is used, the sewing is usually done by quick-running small machines, such as the Yankee or Union; each of these machines is capable of sewing more than 2,000 bags per day. For the heavier types of cloth, such as sacking, S, Fig. 32, the sewing is almost invariably done by the Laing or overhead sewing machine, the general type of which is illustrated in Fig. 49, and made by Mr. D. J. Macdonald, South St. Roque's Works, Dundee. This is an absolutely fast stitch, and approximately 1,000 bags can be sewn in one day.
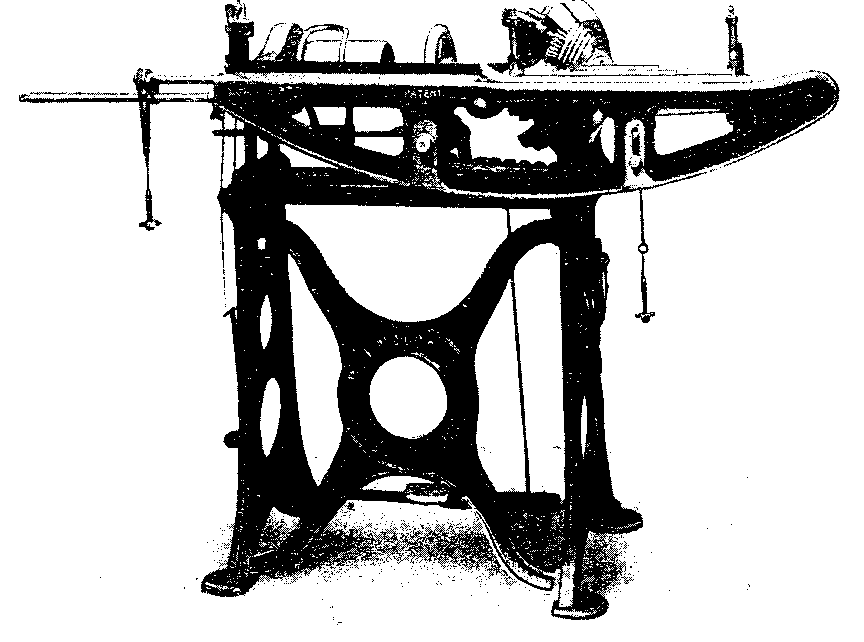
FIG. 49 OVERHEAD (LAING) SACK SEWING MACHINE By permission of Mr. D. J. Macdonald
The distinctive marks in bags for identification often take the form of coloured stripes woven in the cloth, and as illustrated at S, Fig. 32. It is obvious that a considerable variety can be made by altering the number of the stripes, their position, and their width, while if different coloured threads appear in the same cloth, the variety is still further increased.
Many firms, however, prefer to have their names, trade marks, and other distinctive features printed on the bags; in these cases, the necessary particulars are printed on the otherwise completed bag by a sack-printing machine of the flat-bed or circular roller type. The latter type, which is most largely used, is illustrated in Fig. 50. It is termed a two-colour machine, and is made by Mr. D. J. Macdonald, Dundee; it will be observed that there are two rollers for the two distinct colours, say red and black. Occasionally three and four-colour machines are used, but the one-colour type is probably the most common.
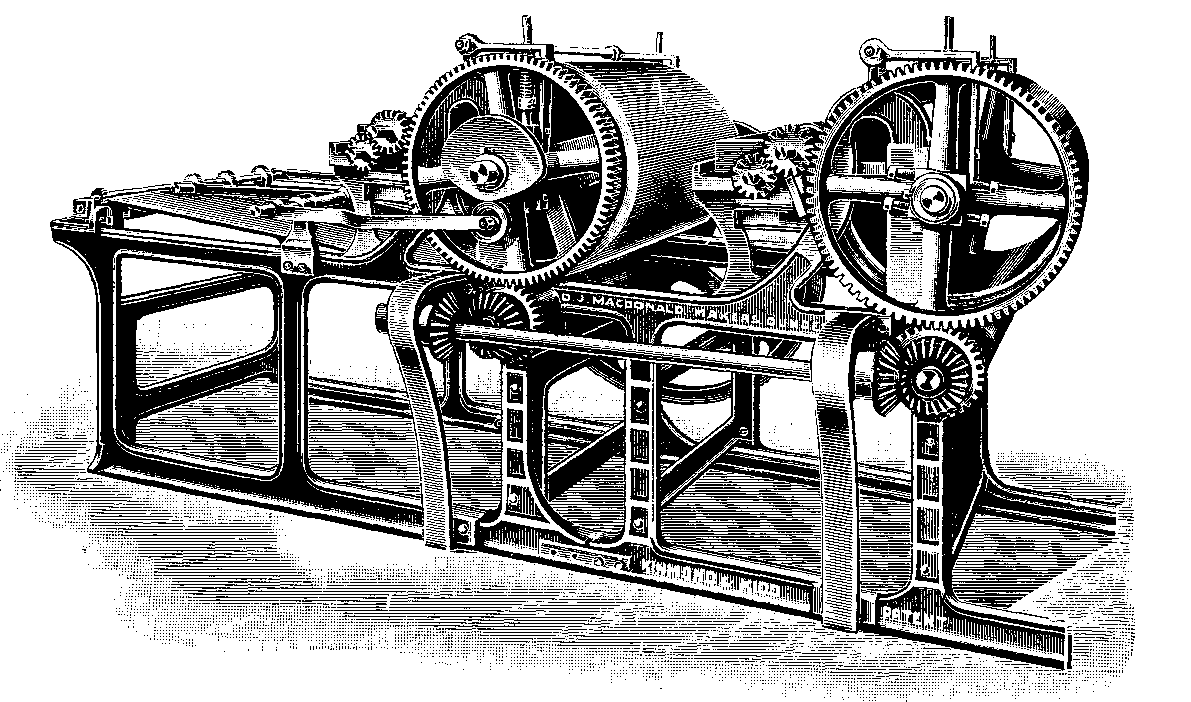
FIG. 50 SACK PRINTING MACHINE By Permission of Mr. D. J. Macdonald.
The ownership of the bags can thus be shown distinctly by one of the many methods of colour printing, and if any firm desires to number their bags consecutively in order to provide a record of their stock, or for any other purpose, the bags may be so numbered by means of a special numbering machine, also made by Mr. D. J. Macdonald.
The last operation, excluding the actual delivery of the goods, is that of packing the pieces or bags in small compass by means of a hydraulic press. The goods are placed on the lower moving table upon a suitable wrapping of some kind of jute cloth; when the requisite quantity has been placed thereon, the top and side wrappers are placed in position, and the pumps started in order to raise the bottom table and to squeeze the content between it and the top fixed table. From 1 1/2 ton to 2 tons per square inch is applied according to the nature of the goods and their destination. While the goods are thus held securely in position between the two plates, the wrappers a sewn together. Then specially prepared hoops or metal bands are placed round the bale, and an ingenious and simple system, involving a buckle and two pins, adopted for fastening the bale. The ends of the hoop or band are bent in a small press, and these bent ends are passed through a rectangular hole in the buckle and the pins inserted in the loops. As soon as the hydraulic pressure is removed, the bale expands slightly, and the buckled hoop grips the bale securely.
Such is in brief the routine followed in the production of the fibre, the transformation of this fibre, first into yarn, and then into cloth, and the use of the latter in performing the function of the world's common carrier.
INDEX
ACCUMULATOR
Assorting jute fibre.
BAG-MAKING
Bale opener
opening
Baling cloth
house
press
station
Bast layer (see also Fibrous layer)
Batch
Batchers
Batching
apparatus
carts or stalls
Batch-ticket
Beamer's lease
Beaming
(dry) direct from bank,
Blending
Bobbin winding
Bojah
Botanical features of jute plants
Breaker card
Brussels carpet
Bundle of jute.
CALCUTTA, jute machinery introduced into
Calender
finish
Calenderoy
Carding
Card waste
Cargoes of jute
Chest finish
Clasp-rods
Conditioning fibre
Cops
Cop winding
Corchorus capsularis
clitorius
Crisping and crisping machines
Cropping machine
Cultivation of jute
Cutting knife for jute fibre
Cuttings.
DAMPING machine
Defects in fibre and in handling
Designs or weaves
Differential motion
Dobby loom
Draft
Drafting
Drawing
frames
different kinds of
Drawing-in
Dressing and dressing machine
Drum
Drying jute fibre
Dust shaker.
EAST India Co.
Exports of jute from India.
FABRICS
Faller
Farming operations
Fibres,
the five main
imports of jute.
Fibrous layer
Finisher card
Finishing
folding machine.
Gaiting
Glazed finish
Grading jute fibre
Gunny bags.
Hand batching
Harvesting the plants
Height of jute plants
Hydraulic mangle
press.
Identification marks on bags
Imports of jute.
Jacquard loom
Jute crop
exports from India
fabrics
fibre, imports of
industry
knife
plants, botanical and physical features of
cultivation of
height of
marks.
Laddering
Ladders
Lapping machine
Linking machine
Linoleum
Looms
Lubrication of fibre.
Machine batching
Machinery for jute manufacture introduced into Calcutta
Mangle finish
(hydraulic)
Marks of jute (see jute marks)
Maund
Measuring and marking machine
machine for cloth
the warp
Methods of preparing warps
Multiple-colour printing machines.
Numbering machine for bags.
Opening jute heads
Overhead runway systems
sewing machine (Laing's).
Packing goods
Physical features of jute plants
Pin-lease
Plaiting machine
Plants, thinning of
weeding of
Ploughs for jute cultivation
Point-paper designs
Porcupine feed
Printing machine.
Reach
Reeling
Retting
Roller-feed
Rolls
Root-comber
opener
Round-thread finish
Rove
Roving frame
Roxburgh, Dr.
Sack-cutting frame, semi-mechanical
Sack making
printing machine
Sand bags
Seed
per acre, amount of
sowing of
Sewing machines
Shell-feed
Short-tell
Snipping machine
Softening machines
Spinning
Spool or roll winding
Spools (see Rolls)
Standard bale
Starching (see Dressing)
Steeping (see Retting)
Striker-up (see Batcher)
Stripping
Systems.
Teazer
Tell (of yarn)
Thinning of plants
Thrum
Time for harvesting the plants
Tube-twisters
Twist
Twisting
Two-colour printing machine
Tying-on
Typical jute fabrics.
Union Or Yankee sewing machine
Unloading bales of jute from ship.
Variations in jute
Varieties of jute fibre
plants.
Warp
Warp dressing (see Dressing)
Warping, beaming and dressing
mill
Washing
Waste
teazer
Weaves or designs
Weaving
Weaver's lease
Weeding of plants
Weft
winding
Wilton carpet
Winding (bobbin) machine
from hank
(large roll) machine
(ordinary size from hanks) machine
rolls and cops
World's great war.
Yankee or Union sewing machine
Yarn table
Yield of fibre.
Printed by Sir Isaac Pitman & Sons, Ltd., Bath, England
Advertisement: Thomas Hart, LTD.; DAVID KEAY & LESLIE"
Advertisement: ROYLES LIMITED.
Advertisement: D. J. MACDONALD C.E., M. I.M. ECH.E.
Advertisement: ROBERTSON & ORCHAR, LTD.
Advertisement: WHITE, CHILD & BENEY, LIMITED
Advertisement: THE BRITISH NORTHROP LOOM CO., LTD.
NORTHROP AUTOMATIC LOOM as used in the jute trade Models for Cotton, Woolen, and Worsted, jute, linen, silk, etc. All sizes from 28" to 120"
Advertisement: FREDERICK SMITH & CO.
Advertisement: THE SKEFKO BALL BEARING CO., LTD.
Advertisement: PITMAN HANDBOOKS: ARITHMETIC
Advertisement: PITMAN HANDBOOKS: BOOK-KEEPING & ACCOUNTANCY
Advertisement: PITMAN HANDBOOKS: BUSINESS TRAINING
Advertisement: PITMAN HANDBOOKS: CIVIL SERVICE
Advertisement: PITMAN HANDBOOKS: ENGLISH, HISTORY
Advertisement: PITMAN HANDBOOKS: ECONOMICS, BANKING
Advertisement: PITMAN HANDBOOKS: INSURANCE, SHIPPING, INCOME TAX
Advertisement: PITMAN HANDBOOKS: ADMINISTRATION, ADVERTISING
Advertisement: PITMAN HANDBOOKS: HANDBOOKS, REFERENCE
Advertisement: PITMAN HANDBOOKS: COMMODITIES, LAW
Advertisement: PITMAN HANDBOOKS: FRENCH
Advertisement: PITMAN HANDBOOKS: GERMAN, SPANISH
Advertisement: PITMAN HANBOOKS: ITALIAN, SHORTHAND
Advertisement: PITMAN HANDBOOKS: SHORTHAND DICTIONARIES, PHRASES
Advertisement: PITMAN HANDBOOKS: SHORTHAND SPEED PRACTICE, READING
Advertisement: PITMAN HANDBOOKS: TEACHING, TYPEWRITING, PERIODICALS
Advertisement: HENRY TAYLOR & SONS, LTD., PITMAN'S BOOKS
Advertisement: THOS. BROADBENT & SONS, LTD.